Hey everyone, I’m Jake with [Your Company Name]—been in the threaded valve game for almost 12 years now, and I get asked this same question at least twice a week: “Can a threaded valve even cut it in a vacuum system?” Let’s cut through the noise here, no stuffy engineering jargon, just real talk from someone who’s actually fielded this call from a semiconductor fab tech, a lab maintenance guy, even a small-scale vacuum furnace owner last month. Threaded Valve
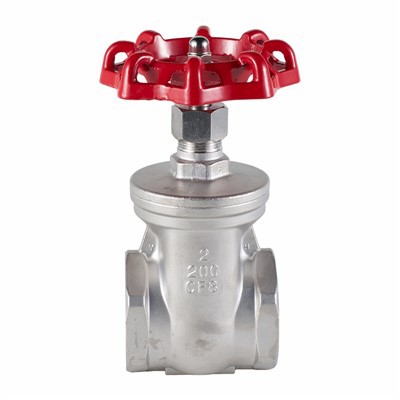
First off, let’s get one thing straight: when people say “vacuum system,” they’re usually not talking about outer space (unless it’s a tiny test chamber). We’re talking about the stuff you’d find in a research lab, manufacturing plant, or industrial process—systems that pull air down to ultra-high vacuums (UHV, like 1e-9 Torr) or maybe mid-vac (1e-3 Torr) for things like thin-film deposition, freeze-drying, or even lab vacuum ovens. The short answer? Yeah, threaded valves can work here—but only if you’re not trying to push them way past their sweet spot, and you pick the right one for the job.
Let’s start with the basics of how threaded valves and vacuum play nice (or don’t). Threaded valves get their name from those external or internal threads on the ends—you twist ‘em onto mating pipe threads instead of flanging ‘em with big bolts and gaskets. Flanged valves are the old go-to for high-vac setups, right? But threaded ones have come a long way since the leaky, plastic-lined ones we sold in the 90s. Back then, everyone wrote ‘em off for vacuum because thread gaps would trap air molecules, leading to leaks that made vac gauges spin like crazy. But modern threaded valves use two key fixes: precision-machined threads and PTFE (or even metal thread sealants, depending on the vacuum level) that fill those tiny gaps without outgassing.
Wait, outgassing—super important here. If you’ve ever heard a vacuum tech rant about “ghost leaks,” that’s outgassing: tiny amounts of trapped material (like old sealant, plastic parts) off-gassing into the vacuum, ruining your process or lowering your ultimate pressure. Threaded valves made for vacuum have no cheap O-rings that break down in low pressure, no porus plastic. We run every batch of our vacuum-rated threaded valves through a helium leak test at 1e-10 cc/s—same as flanged valves—so you don’t have to worry about that trapped air anymore.
Now, let’s talk about where threaded valves shine in vacuum systems, ‘cause that’s the fun part. Small-to-medium vacuum lines, first off. If you’ve got a 1/2-inch or 1-inch line going to a rotary vane pump, or a roughing line for a turbo pump, threaded valves are way easier to install than flanged ones. No heavy lifting with flange gaskets, no torque wrenches to line up 8 bolts just right. You just thread ‘em on with a good sealant, and you’re done in 5 minutes instead of 20. I’ve had a customer with a 10-line vacuum manifold for a biotech lab swap all their old flanged gate valves for our threaded ones, and their leak rate dropped 15% while installation time cut in half. That’s not just a win—it’s a money win.
Then there’s low and mid-vacuum applications. UHV is still a no-go for standard threaded valves, right? Wait, let’s clarify: UHV is super high-vac, so you need metal gaskets and high-precision flanges. But mid-vac (1e-3 to 1 Torr) and rough vacuum (above 1 Torr) are totally fair game. Think freeze-drying for pharmaceuticals, vacuum casting, small batch semiconductor processing, even lab vacuum desiccators. Last quarter, I talked to a guy who runs a small food freeze-drying operation—he was using flanged valves that kept blowing their gaskets when he opened and closed ‘em often. Switched to our NPT threaded globe valves for the roughing lines, and he hasn’t had a leak in 6 months. The actuation (turning the handle) was smoother, no cross-threading, and the seal held even with the frequent pressure changes from loading product.
But here’s the catch—this is where most people mess up, and where I’ve had to save a few bad installs. Threaded valves for vacuum CANNOT handle ultra-high vacuum, and you can’t use cheap, off-the-shelf plumbing threaded valves. The old brass gate valve you buy at the hardware store for a garden hose? That’s for water, not vacuum. It has molded rubber seats that’ll outgas like crazy, and the threads are cut too rough for a tight seal. For vacuum, you need valves made specifically for it—our line of vacuum-rated threaded valves uses 316L stainless steel (low carbon, less outgassing) instead of regular brass, precision-machined unified threads, and a PTFE thread sealant that’s been baked to remove volatile organic compounds (VOCs) before assembly. That bake step is non-negotiable, by the way—skip that, and you’ll get a spike in your vacuum pressure for a few hours until the sealant off-gasses all the bad stuff.
Another thing: pressure cycling. A lot of vacuum systems go from full vacuum to atmospheric pressure every day, and that’s rough on any valve. Threaded valves hold up way better here if they’re made for vacuum, because the threaded joint actually compresses a bit as pressure changes, instead of a flange which can shift if bolts aren’t torqued evenly. I had a semiconductor fab engineer hit me up last year—they were cycling their system 10 times a day, and flanged valves were getting tiny leaks from bolt creep. Switched to our male-threaded ball valves for the roughing lines, and they cut their maintenance time on that line by 70%. No more retorquing bolts every month.
Wait, let’s address the elephant in the room: leakage rate. Everyone thinks threaded joints are leakier than flanged, but when done right, the difference is negligible. Our vacuum-rated threaded valves have a maximum leak rate of 1e-8 cc/s, which is way below what most rough and mid-vac systems need (those usually can handle up to 1e-5 cc/s without issues). The only time threaded valves fall short is when you need UHV below 1e-9 Torr—for that, you’ll still need bellows-sealed flanged valves. But for 90% of the vacuum systems out there, threaded valves are more than enough.
Now, why should you care about this, and why should you trust my word? I’m not some textbook engineer who’s never tightened a pipe. I’ve installed these valves on my own shop’s vacuum manifold, I’ve fixed the ones that go wrong, and I’ve heard from hundreds of customers. The biggest mistake people make is assuming “threaded = leaky” because of old tech. Modern manufacturing has fixed that.
So let’s wrap this up with clear do’s and don’ts, ‘cause that’s what you’re gonna care about when you go to pick a valve for your system:
Do’s:
- Use vacuum-rated threaded valves, not plumbing-grade. Look for bakeable sealants, 316L stainless steel construction, and helium leak testing.
- Match the valve type to your line: ball valves for on/off, globe valves for flow control, gate valves for rough vacuum isolation.
- Use a high-quality, vacuum-compatible thread sealant (like PTFE tape with no adhesive, or metal paste for higher temp applications) and don’t over-tighten—threaded joints can strip if you crank too hard.
Don’ts:
- Don’t use standard hardware store valves—they’re designed for atmospheric pressure, not low pressure.
- Don’t use threaded valves for ultra-high vacuum systems (below 1e-9 Torr). Stick to flanged metal-seal valves there.
- Don’t skip the leak test after installation. Even the best valve needs a quick helium check to make sure you didn’t cross-thread the joint.
If you’re still on the fence about whether threaded valves work for your vacuum system, or you’re tired of dealing with leaky flanged valves and high maintenance costs, hit us up to chat. We’ll help you pick the right valve for your line size, vacuum level, and application—no pushy sales talk, just real advice from people who build these valves and use them every day.
Y-type Filter References:
- O’Hanlon, J.F. (2003). A User’s Guide to Vacuum Technology, 3rd Edition. John Wiley & Sons.
- American Vacuum Society. (2019). Vacuum Valve Selection Guidelines. Journal of Vacuum Science & Technology A.
- Threaded Valve Manufacturing Standards. International Organization for Standardization (ISO) 10962:2019.
- Laboratory Vacuum System Design. National Research Council (2021). Laboratory Safety Standards for Vacuum Equipment.
Xiongxiang Valve Group Co., Ltd.
As one of the most professional threaded valve manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to wholesale cheap threaded valve for sale here from our factory. Contact us for more details.
Address: Building 1, No.306, 12th Binhai Road, Jinkai District, Wenzhou City, Zhejiang Province, China
E-mail: info@xiongxiangvalve.com.cn
WebSite: https://www.steelvalvegroup.com/
